
China has become a major sourcing base for precision motor components, including the Armature Shaft. Its manufacturers serve power tools, automotive motors, household appliances, pumps, and industrial equipment. Yet “top” should not mean the largest factory alone. It should mean consistent performance, traceable processes, and honest technical communication.
Manufacturing expert Dr. Geoffrey Boothroyd expressed a useful principle: “Design must consider manufacturing from the beginning.” This idea fits Armature Shaft purchasing closely. A reliable supplier should review shaft drawings before production. It should check steel grade, diameter tolerance, keyway accuracy, runout, surface hardness, and balancing requirements. CNC turning creates the profile. Grinding controls the final dimensions. Heat treatment protects wear-prone areas. Inspection records should connect each batch with measurable results.
Strong Chinese manufacturers usually provide material certificates, process inspection reports, sample approval, and stable export packaging. Some also support custom splines, knurling, grooves, and stepped shafts. Ask about production capacity, not only quoted price. Ask how rejected parts are isolated. Ask whether the supplier measures runout after heat treatment. Small questions expose large differences.
The factory floor matters.
A polished website proves little. A clean inspection room proves more. However, even capable manufacturers may show uneven documentation or delayed engineering replies. That weakness deserves attention, not automatic rejection. Buyers should compare verified samples, communication quality, lead time, and corrective-action speed. This outline examines China’s leading Armature Shaft manufacturers through those practical standards, while recognizing that supplier rankings can change with equipment, workforce, and quality discipline.
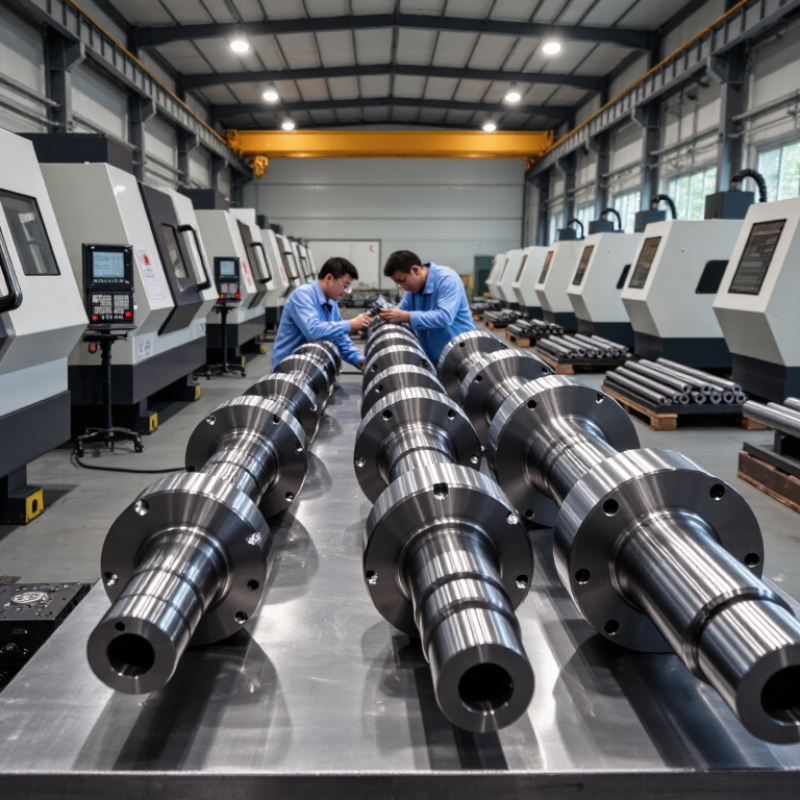
An armature shaft is the rotating steel core that transfers torque from an electric motor to its load. It supports the armature, commutator, bearings, and sometimes a cooling fan. Its diameter may look modest, but small errors can create large operating problems.
Manufacturing quality matters because the shaft must remain straight under speed, heat, and repeated torque. Skilled manufacturers control runout, concentricity, surface hardness, and keyway dimensions during machining. Dynamic balancing is also essential. A shaft with uneven mass can produce vibration, bearing wear, and unpleasant noise. In practical inspections, a smooth surface is not enough. A shaft may look perfect while hidden stress or poor heat treatment weakens it.
Reliable producers use verified steel grades, controlled forging or bar-stock processes, and traceable inspection records. They measure critical areas with calibrated instruments, then test hardness, dimensions, and balance. Some also inspect for cracks after machining. These steps increase consistency across production batches.
Quality decisions are rarely simple. A harder surface may improve wear resistance, yet excessive hardness can reduce toughness. Tight tolerances improve alignment, but they may raise manufacturing costs. Even experienced teams can miss a minor defect when inspection depends on one method. That is why responsible manufacturers combine process control, dimensional checks, and application-specific testing before shipment. A shaft designed for a compact appliance should not automatically follow the same standards as one used in industrial equipment.
An armature shaft is the rotating shaft that supports the armature core, commutator or rotor assembly, and bearings in many electric motors and generators. The following table summarizes the principal manufacturing dimensions used to evaluate armature-shaft quality without presenting company or brand rankings.
| Evaluation Dimension | Typical Industry Data or Practice | Why Manufacturing Quality Matters |
|---|---|---|
| Primary Function | Transmits torque from the rotor or armature to the driven equipment while maintaining the position of the laminated core, commutator, gears, fans, and bearings. | Incorrect shaft geometry can create eccentric rotation, excess vibration, bearing load, noise, and premature motor failure. |
| Common Materials | Frequently selected materials include medium-carbon steel such as C45 or AISI 1045, alloy steel such as 40Cr or AISI 5140/4140, and corrosion-resistant stainless steels such as 17-4 PH when application conditions require them. | Material selection determines tensile strength, fatigue resistance, machinability, hardenability, corrosion resistance, and compatibility with the required heat treatment. |
| Manufacturing Route | A common route is bar or forged-stock preparation, turning, drilling or milling, heat treatment, grinding of critical journals, deburring, cleaning, inspection, and final balancing when required. | Each stage affects dimensional stability. Poor sequencing or inadequate process control may cause distortion, surface damage, burrs, or inconsistent bearing fits. |
| Dimensional Accuracy | Bearing seats, seal diameters, keyways, splines, and commutator locations are normally controlled according to the engineering drawing and the applicable fit system. ISO 286 is commonly referenced for hole-and-shaft tolerances and fits. | A shaft that is too large may damage bearings during assembly; a shaft that is too small may produce looseness, fretting, slip, or inaccurate rotor positioning. |
| Runout and Concentricity | Runout and coaxiality limits are application-specific and should be stated on the drawing. They are commonly checked with precision V-blocks, centers, dial indicators, or coordinate-measuring equipment. | Excessive runout changes the air gap and bearing loading, producing vibration, uneven brush wear, acoustic noise, and reduced motor efficiency. |
| Surface Finish | Bearing journals and seal-running surfaces are generally ground or finely turned to a drawing-specified Ra value. The required finish depends on bearing type, lubrication, sealing method, and rotational speed. | Excessively rough surfaces can accelerate seal and bearing wear, while unsuitable finishing processes can create grinding burns, waviness, or poor lubricant behavior. |
| Heat Treatment | Normalizing, quenching and tempering, induction hardening, or case hardening may be used. The treatment is selected according to the required core strength, surface hardness, wear resistance, and fatigue life. | Insufficient hardness can cause journal wear and fretting. Excessive hardness or improper treatment may reduce toughness and increase the risk of cracking or distortion. |
| Keyways and Splines | Torque-transfer features may include parallel keyways, involute splines, serrations, or press-fit sections. Their dimensions, flank condition, and positional tolerances should be defined by the drive-system design. | Poorly formed or incorrectly positioned features can cause backlash, stress concentration, assembly difficulty, torque loss, or shaft cracking. |
| Dynamic Balance | Rotor assemblies are balanced as a complete rotating unit when speed and vibration requirements make this necessary. ISO 21940 is widely used as a reference for balancing quality grades and procedures. | Unbalance generates centrifugal force that rises with the square of rotational speed, increasing vibration, bearing fatigue, noise, and the possibility of structural damage. |
| Inspection Methods | Typical checks include dimensional measurement, runout measurement, surface-roughness testing, hardness testing, visual inspection, magnetic-particle or other non-destructive testing where appropriate, and material-certificate review. | A documented inspection plan helps detect cracks, material mix-ups, dimensional drift, heat-treatment problems, and surface defects before assembly or shipment. |
| Bearing Fit and Assembly | The fit depends on which ring rotates, the applied load, operating temperature, speed, and bearing design. Assembly may use controlled pressing, heating, or other methods that avoid impact damage. | An incorrect fit can cause creep, excessive preload, insufficient internal clearance, bearing overheating, or damage to the raceways. |
| Corrosion Protection | Protection may include controlled packaging, rust-preventive oil, phosphate treatment, plating, or material selection suited to the environment. Coatings must not interfere with critical fits unless specifically allowed. | Corrosion can reduce journal dimensions, damage fits, contaminate bearings, and create stress-raising pits that shorten fatigue life. |
| Traceability and Quality Control | A controlled supplier should be able to link the shaft to the drawing revision, material batch, heat-treatment record, inspection results, and nonconformance history. ISO 9001 is commonly used as a quality-management reference. | Traceability supports root-cause analysis, corrective action, repeatability, and reliable production of replacement or high-volume parts. |
| Application-Specific Performance | Required specifications vary with motor speed, torque, power, duty cycle, temperature, load direction, shaft length, rotor mass, and environmental exposure. There is no single universal tolerance or material for every armature shaft. | A shaft designed only for static strength may still fail from fatigue, resonance, fretting, thermal expansion, or inadequate corrosion protection during actual service. |


